Extrusion
Custom Aluminum Profiles
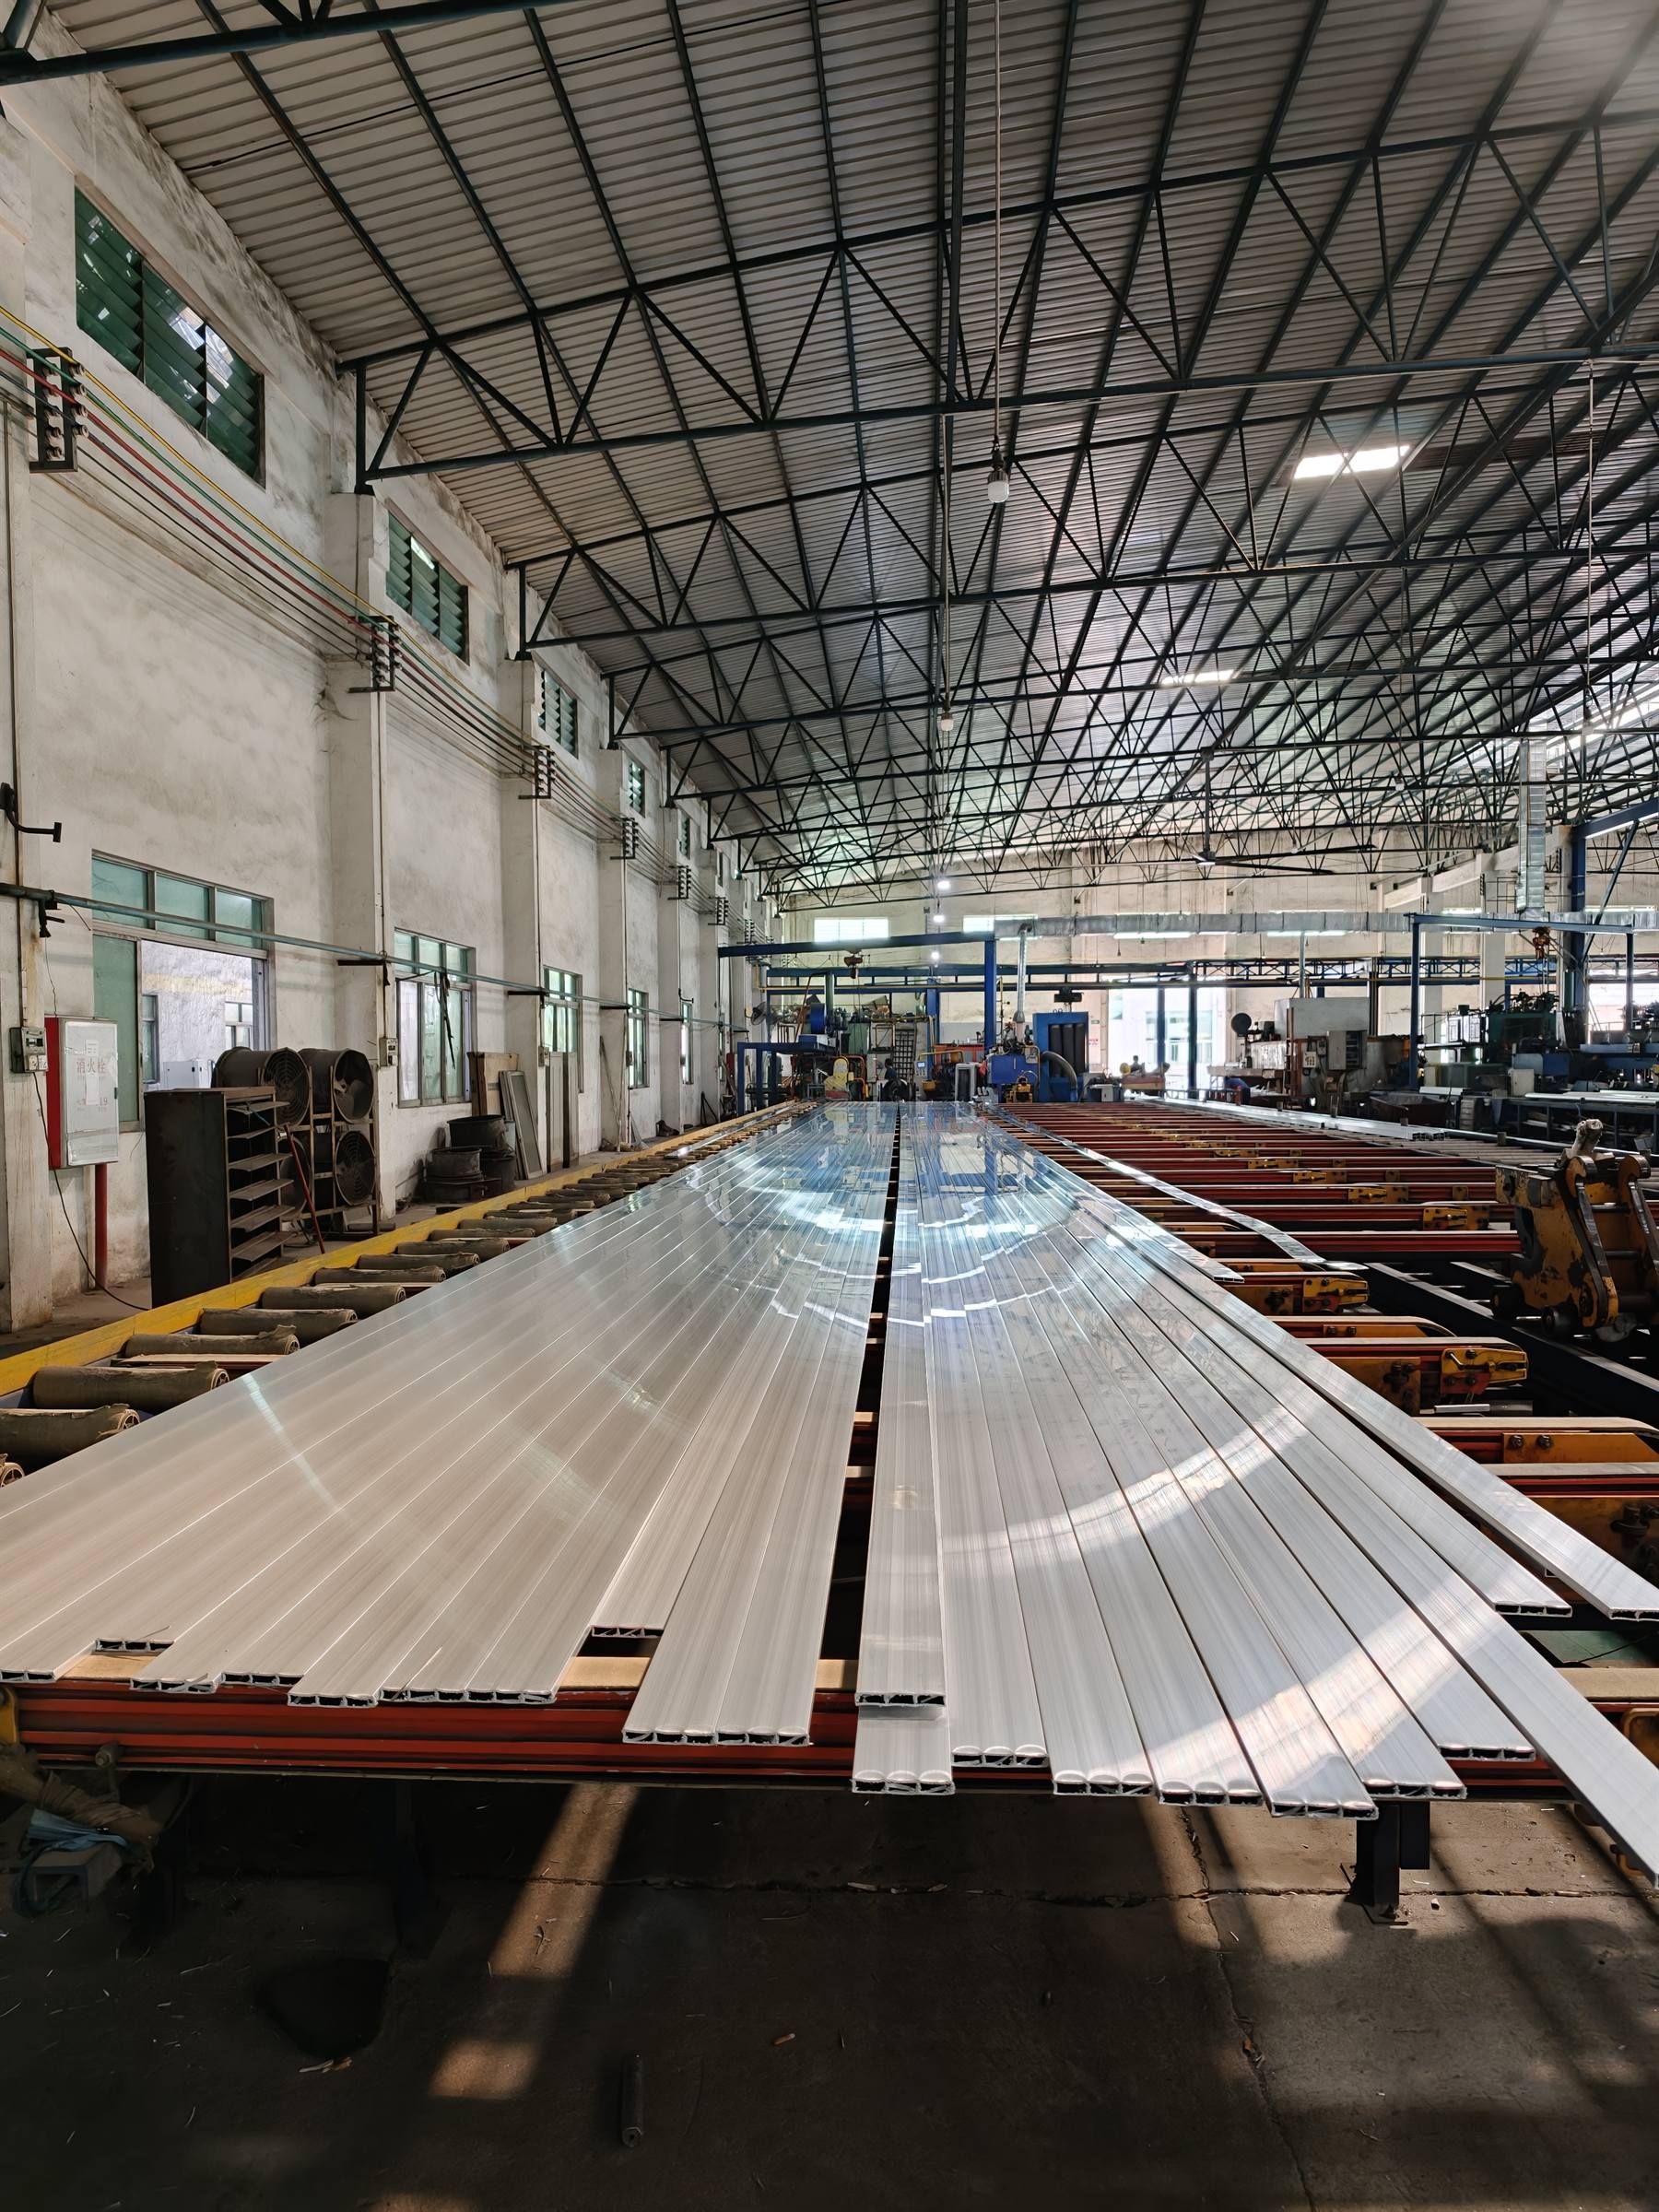
This is the foundation everything else on this site sits on. The presses and the die-cutting sit inside our network, new molds take about five days, and the profile your designer drew is the profile you get.
Specifications
The technical picture
| Alloys | 6063, 6061, 6005 and related 6000-series; tempers including T5 and T6 to suit the application |
|---|---|
| Profile types | Solid, hollow and semi-hollow sections; square and rectangular tube; round tube; angle, channel and flat bar; multi-cavity furniture sections |
| Dimensions | Section size, wall thickness and cut length to your drawing. Send the DWG or DXF and we will confirm what the press can hold. |
| Surface finish | Mill finish, anodizing, powder coating, wood-grain transfer, brushed and matte textures |
| Fabrication | Cut to length, mitre, drilling, punching, bending, CNC machining, welding — supplied as raw bar or as a finished component |
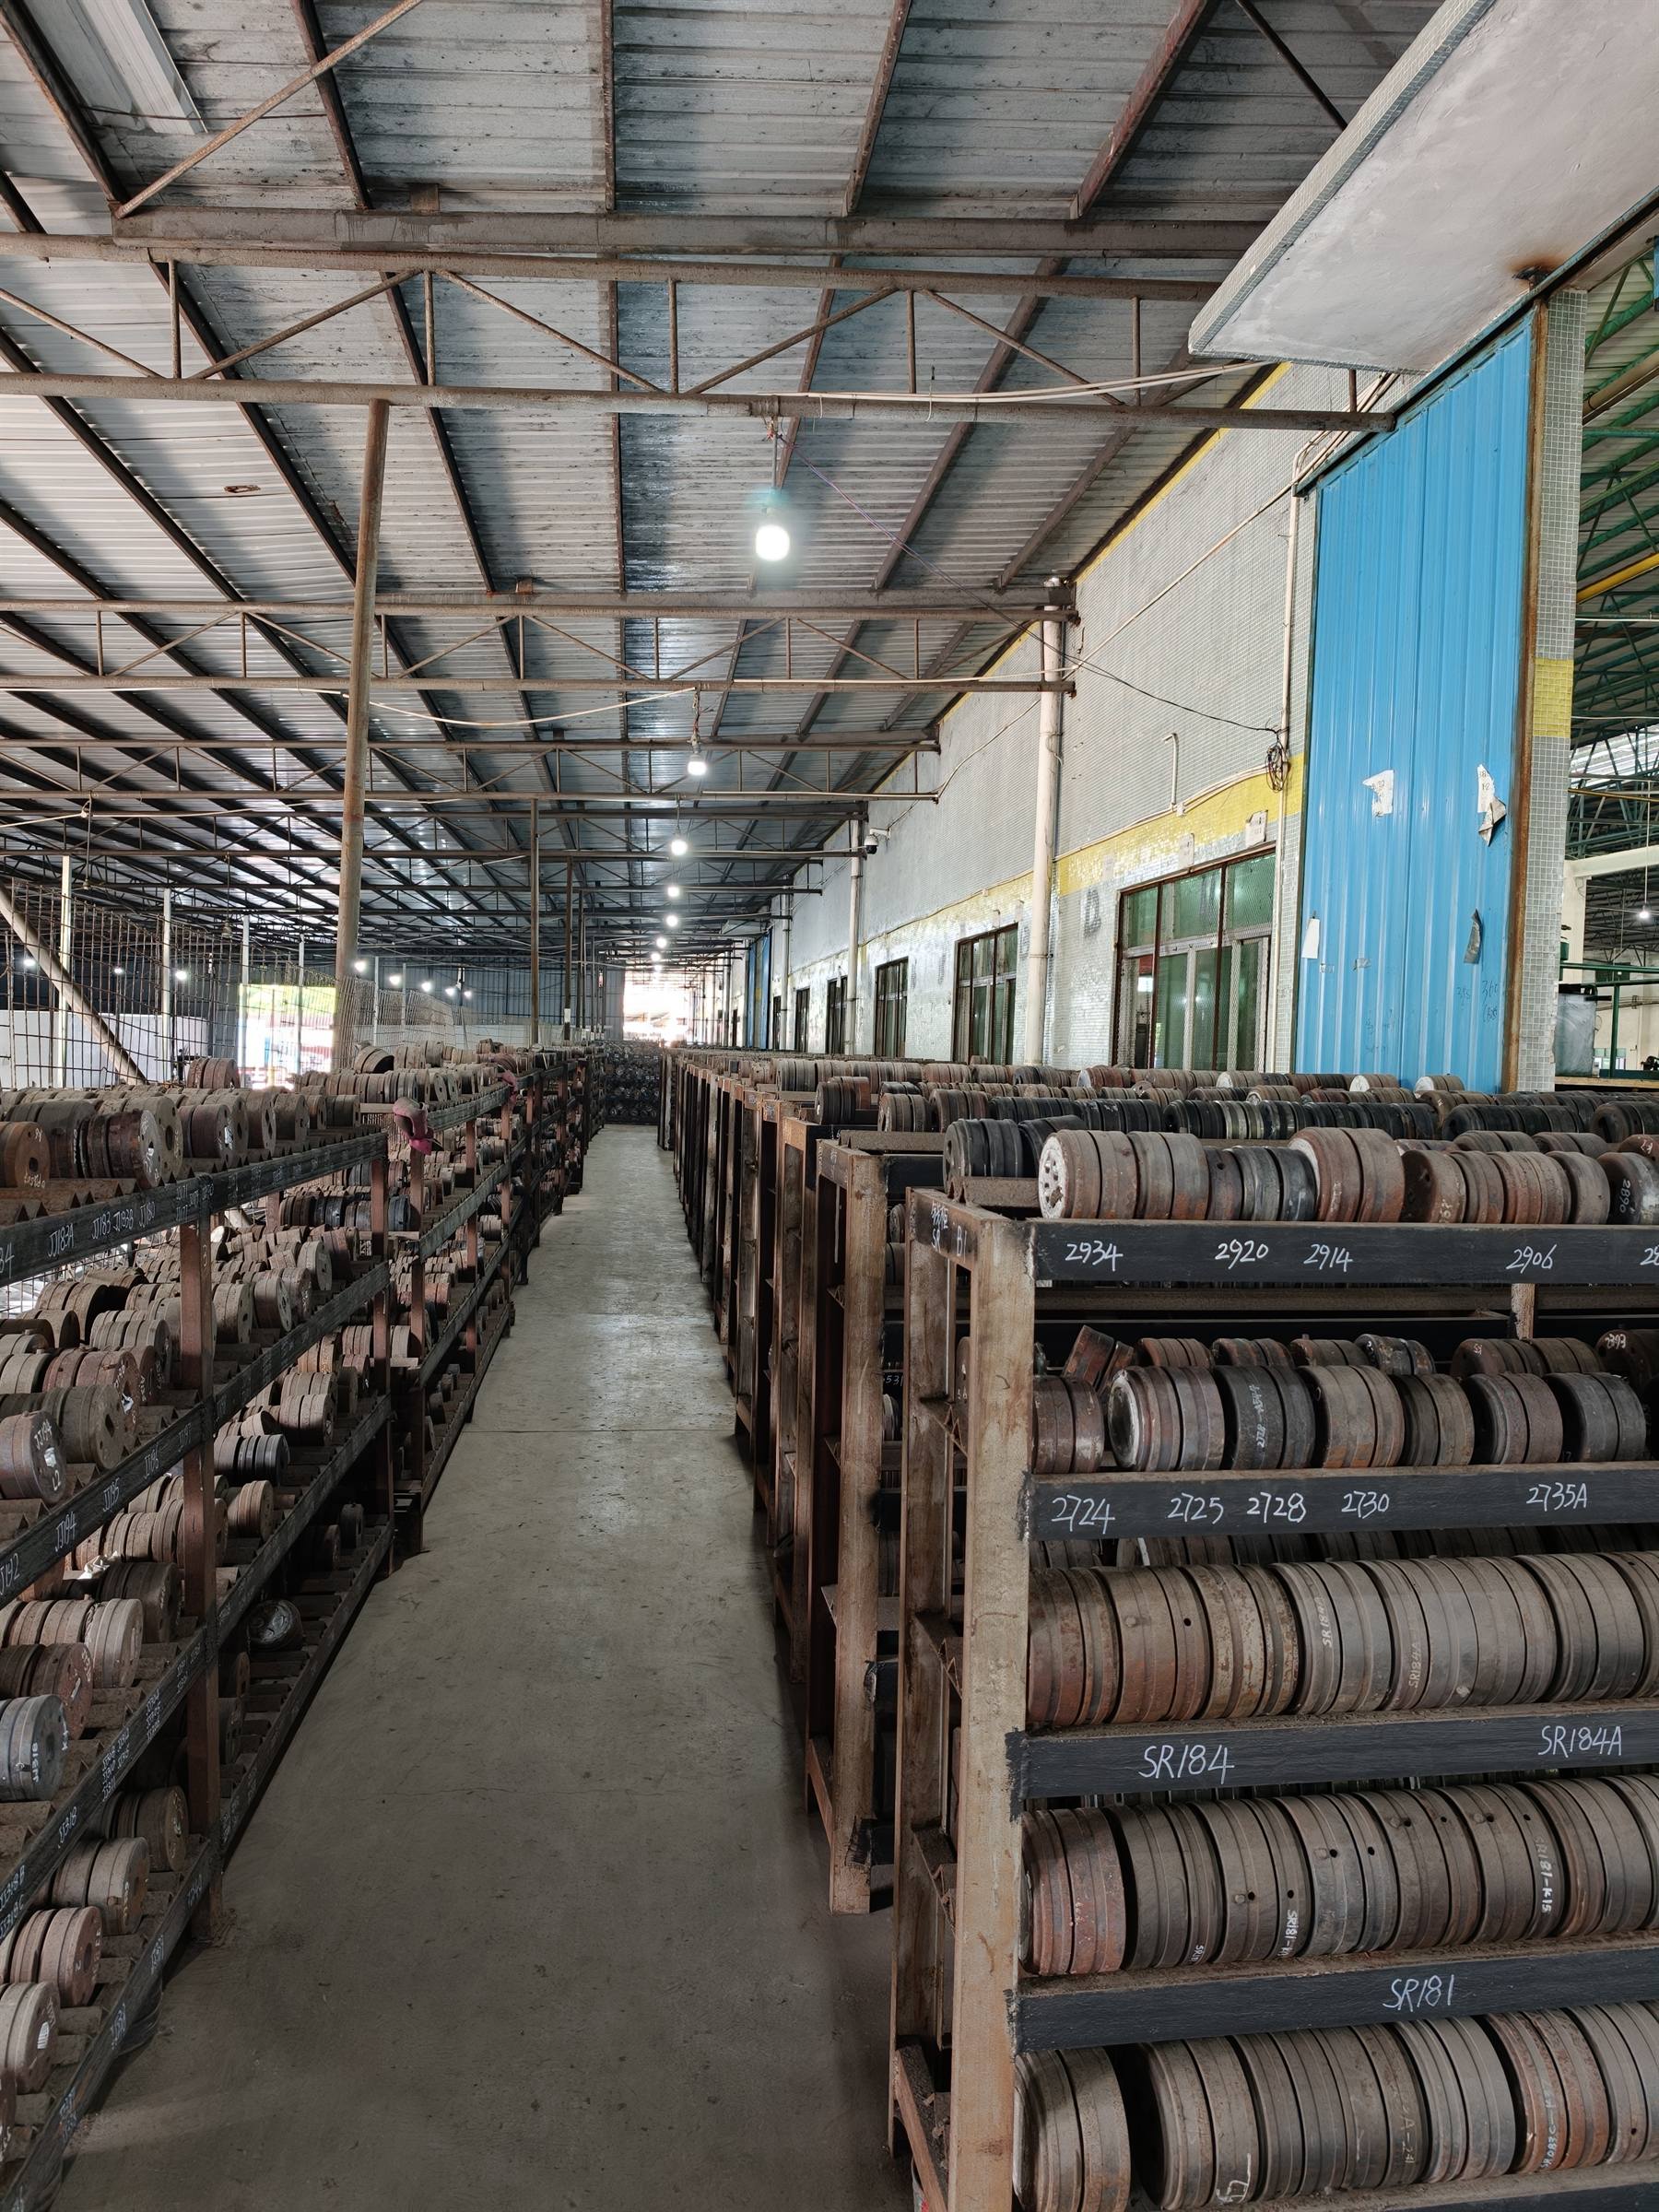
| Tooling | New dies designed and cut in-house. Tooling is catalogued and stored so repeat orders run from the same die. |
| Typical MOQ | Usually quoted in weight rather than pieces — often from a few hundred kilograms per profile per run. Confirmed with your quotation. |
| Packaging | Interleaved and film-wrapped bundles, protective end caps, wooden pallet or crate for export; length-marked and labelled by part number. |
| Customisation | Yes — this is the definition of custom. No stock catalogue required. |
Die development
Tooling is where projects are won or lost
A badly designed die produces a profile that is expensive forever. We would rather spend a week on the cross-section than a year fighting it in production.
Before we cut anything, our engineers review your drawing for wall thickness balance, tongue ratios, corner radii and the finish you are asking the surface to hold. Where a small change will meaningfully reduce cost or scrap, we show you the alternative and let you decide.
Because the die library is ours, a repeat order in year three runs off the same tool as the first one. There is no re-tooling surprise when you re-order.
- Die design reviewed against your drawing before cutting
- Tooling cut in-house in about five days, not outsourced and queued
- Samples 7–15 days after mold approval, off the production die
- Dies catalogued, stored and maintained for repeat runs
Have a cross-section drawing?
DWG, DXF, STEP or PDF. We come back with extrudability feedback, die cost, price per kilogram and lead time.